
ISO 9001 certification and in-house metrology: how CMT builds quality into every atomizer
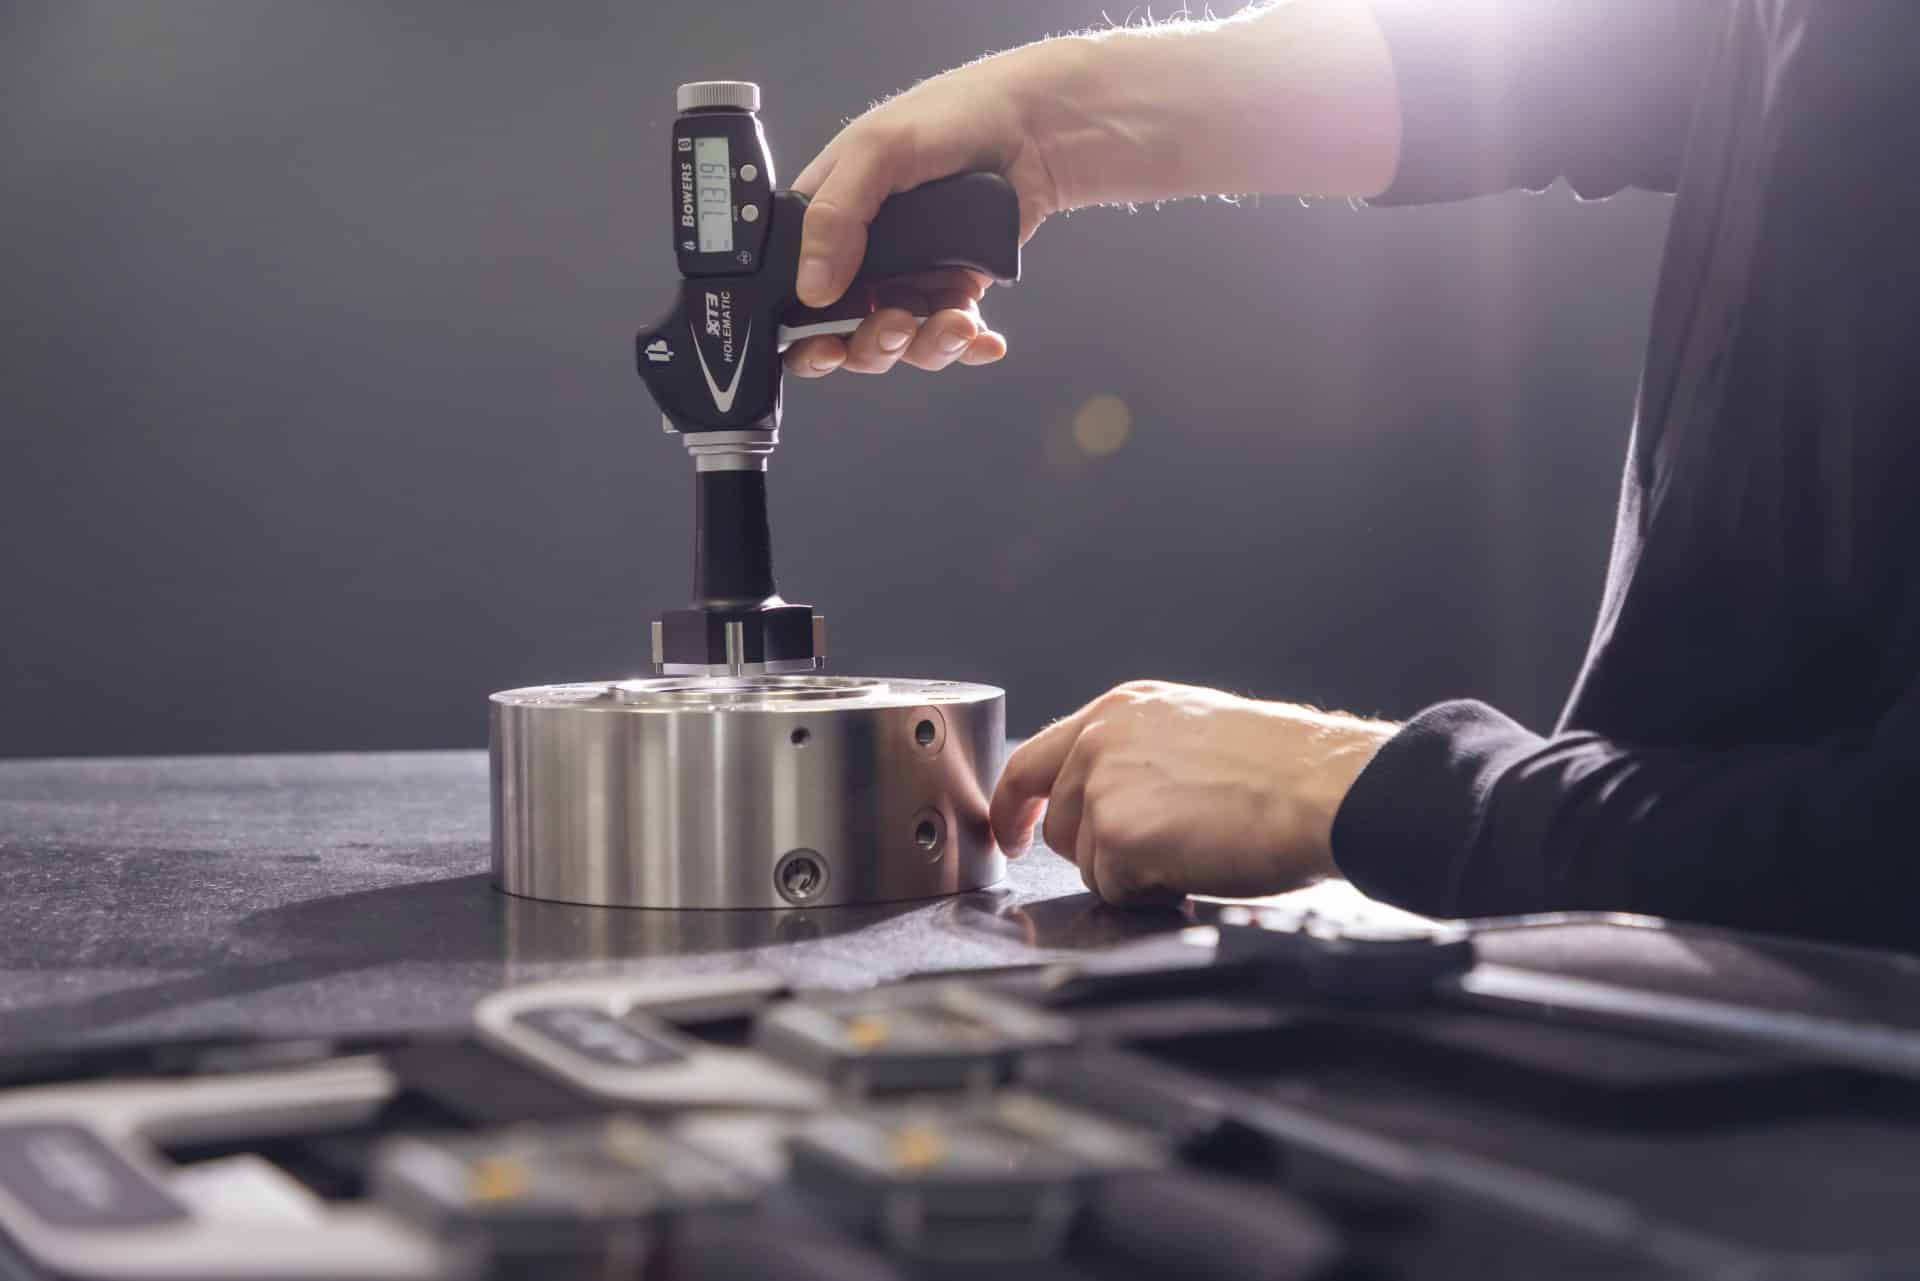
In rotary atomizer manufacturing, quality is not a final checkpoint. It is built step by step, through decisions that guide material acceptance, machining, dimensional checks, assembly, testing, and final release.
For CMT, this approach is supported by ISO 9001 certified atomizer manufacturing and by an in-house metrology process designed to verify critical components before they become part of a machine. The goal is simple: to build reliability into the atomizer before it reaches the spray drying plant.
ISO 9001 is the international standard that defines the requirements for a quality management system. In practical terms, it helps companies work with defined responsibilities, measurable controls, documented procedures and continuous improvement.
Applied to atomizer manufacturing, this means that each production stage follows clear technical and quality criteria. Components are not only manufactured according to drawings: they are checked, recorded and approved through a traceable process.
This is particularly important for industrial rotary atomizers, where high-speed operation, tight tolerances and demanding production environments leave no room for approximation.
CMT’s ISO 9001 quality management system covers the full manufacturing cycle, from procurement to after-sales support. It connects engineering, production and quality control through shared methods and documented inspections.
Controls begin before assembly. Materials and machined parts are checked at different stages, so that potential deviations can be identified early and corrected before they affect the final machine. This applies both to new equipment and to components used for maintenance or refurbishment activities.
This structured atomizer quality control process is especially relevant for sectors where process stability and documentation are essential, including food and pharmaceutical applications. In these industries, reliable atomization depends not only on performance, but also on repeatability, traceability and controlled manufacturing conditions.
The same approach supports CMT’s wider range of rotary atomizers, where each configuration must combine mechanical precision with long-term operational reliability.
One of the key elements of CMT’s quality system is its in-house temperature-controlled metrology room.
Dimensional measurement is highly sensitive to environmental conditions. Even small temperature variations can influence the result when tight tolerances are involved. This is why CMT performs metrology checks in a stable, monitored environment, reducing the risk of measurement distortion and improving inspection consistency.
Inside the metrology room, mechanical parts are verified against the required dimensional specifications before moving to assembly. Shafts, rotating elements, precision-machined parts and other critical components can therefore be checked with the accuracy required for high-speed operation.
Each inspection is documented through control reports, creating a clear record of the measurements performed and the results obtained. This gives CMT visibility over component conformity and supports fast decision-making if a part does not meet the required standard.
These controls also depend on people. CMT invests in the training and professional development of technicians, operators and quality control personnel, with regular updates on regulations, inspection methods, measurement techniques and process management. This keeps quality criteria consistent across departments and strengthens the reliability of the production flow.
Before shipment, every atomizer undergoes functional and performance testing according to defined internal procedures.
These tests verify that the machine operates correctly and complies with the application-specific technical requirements. The results are recorded in dedicated Test Reports, which provide documented evidence of the checks carried out before delivery.
This final validation step turns dimensional controls, assembly checks and operational testing into a documented approval before the atomizer is released to the customer. For demanding sectors such as pharmaceutical processing, this documentation also supports qualification activities and long-term equipment management.
Only after final approval by the quality department is the machine authorized for shipment. The result is an atomizer that has been manufactured, checked and tested through a process designed to reduce non-conformity risk and support long-term performance.
| Quality requirement | How CMT addresses it |
| Controlled production process | ISO 9001-based procedures across the manufacturing flow |
| Dimensional accuracy | In-house metrology in a temperature-controlled room |
| Component conformity | Inspections before assembly and final validation |
| Full traceability | Measurement records and control reports |
| Reduced non-conformity risk | Checks from material acceptance to final release |
| Verified machine performance | Functional testing and dedicated Test Reports |
| Long-term reliability | Precision checks, trained personnel and consistent manufacturing criteria |
By combining certified procedures, in-house measurement capabilities, trained teams and documented testing, CMT builds atomizer reliability and precision into each stage of production.
Quality is not added at the end. It is engineered, measured and verified throughout the entire manufacturing process.
For more information about CMT atomizers, quality procedures and application-specific requirements, contact the CMT team.
